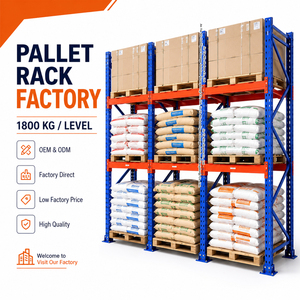
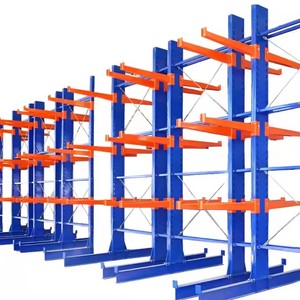
Q1: How does an electric mobile racking system work?
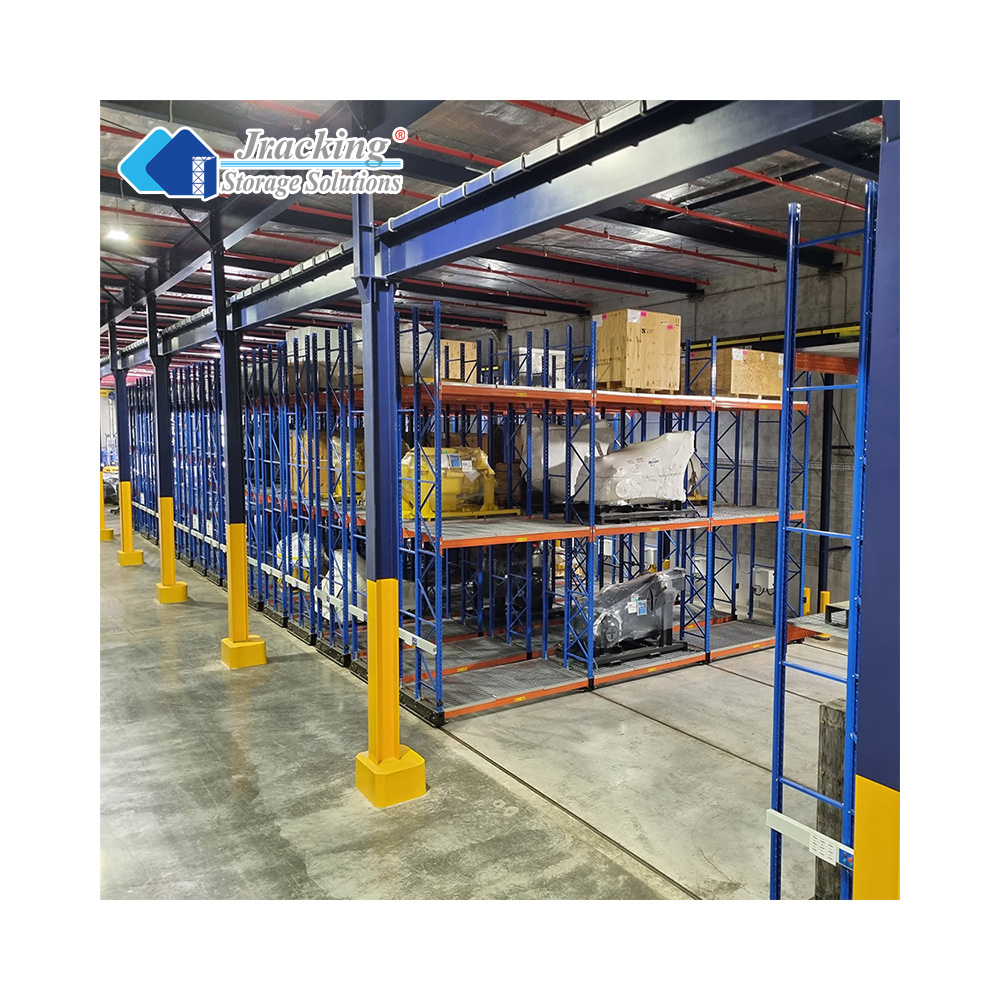
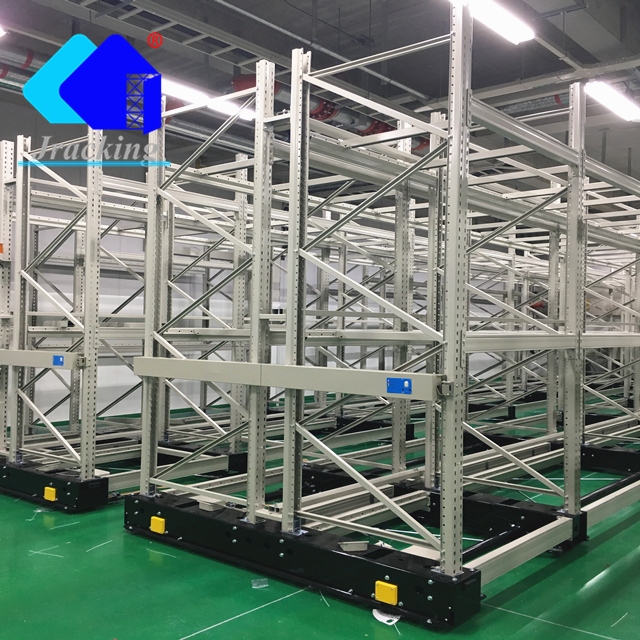
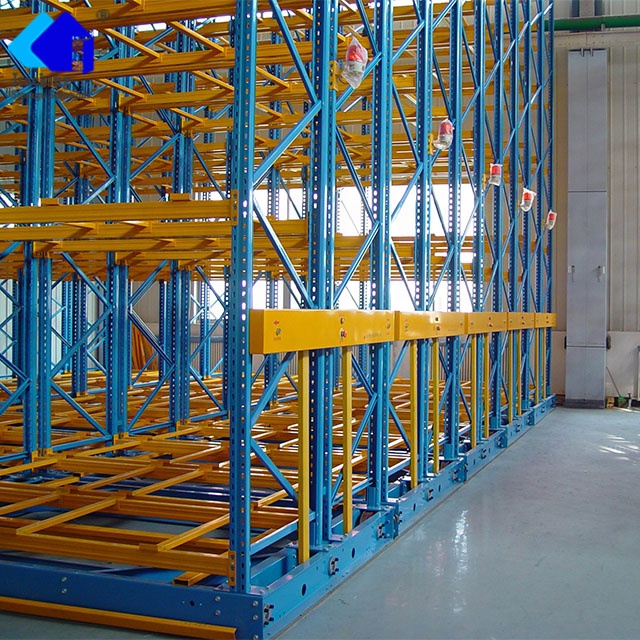
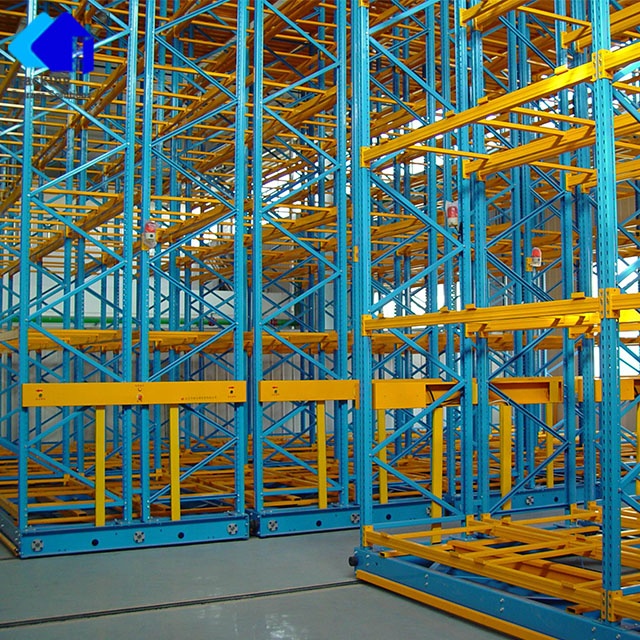
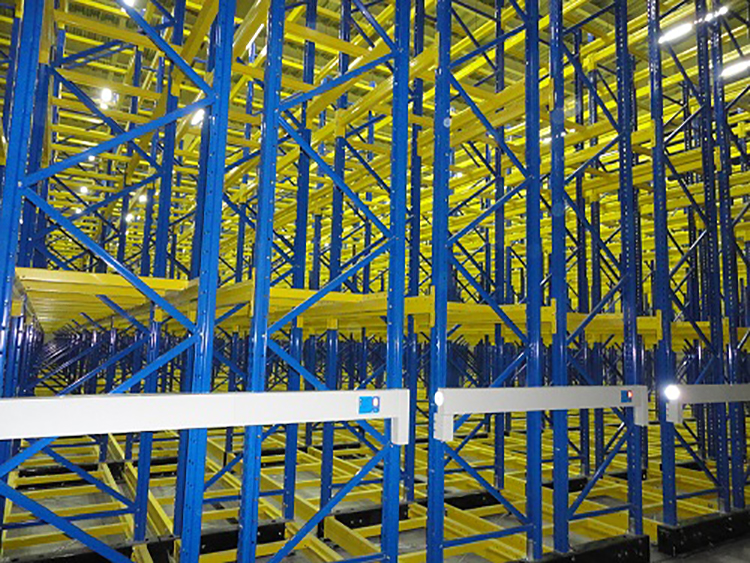
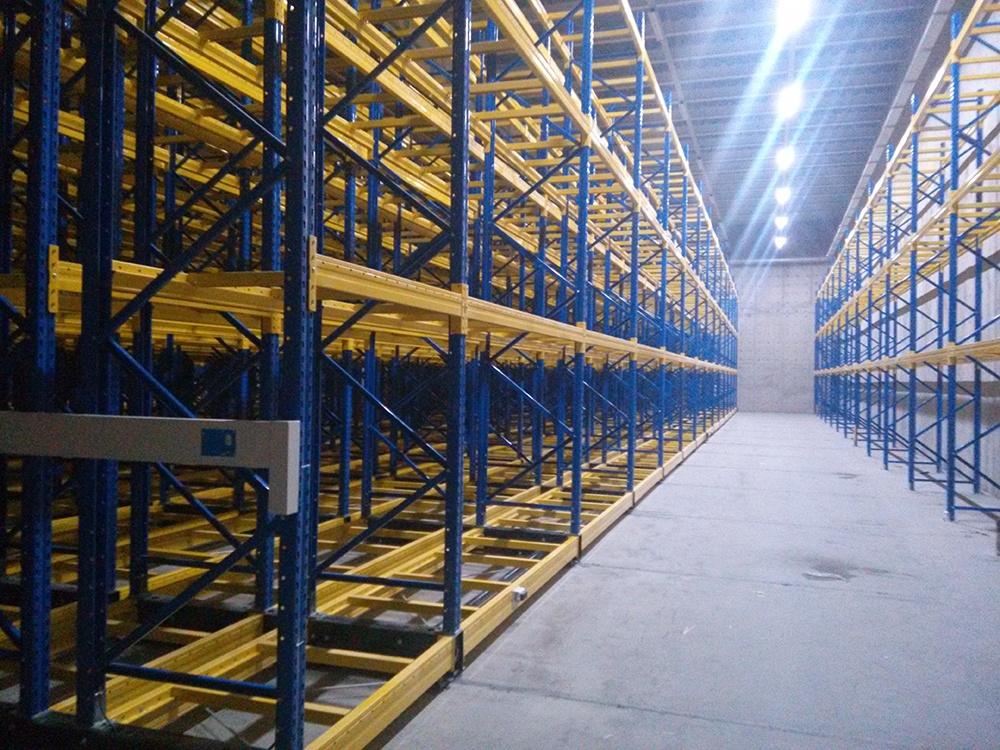
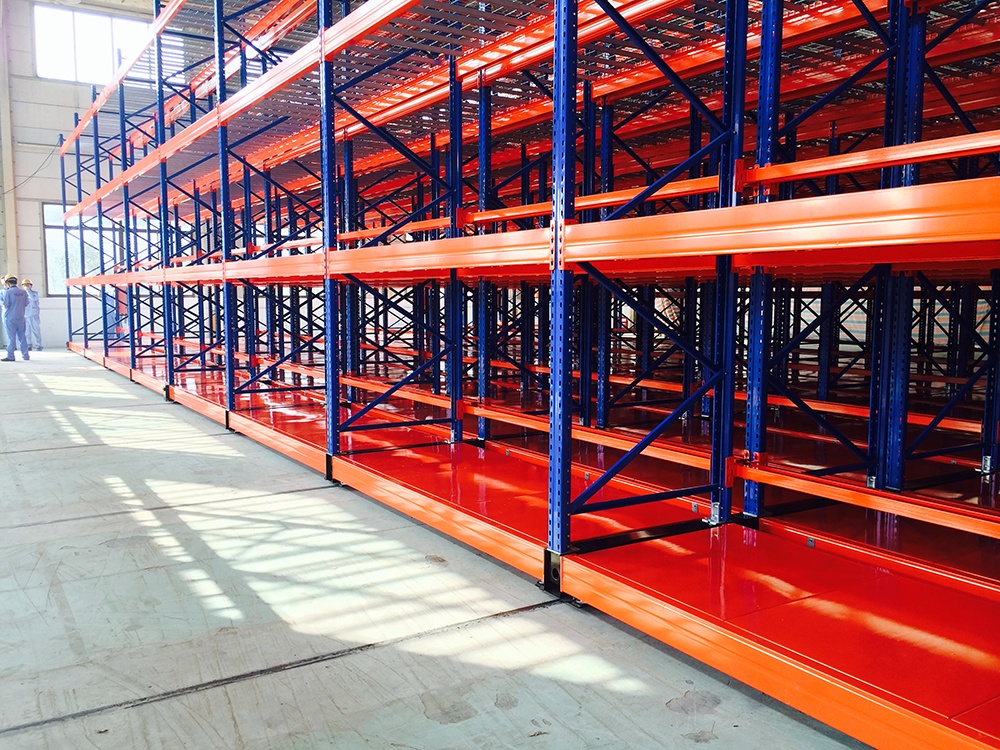
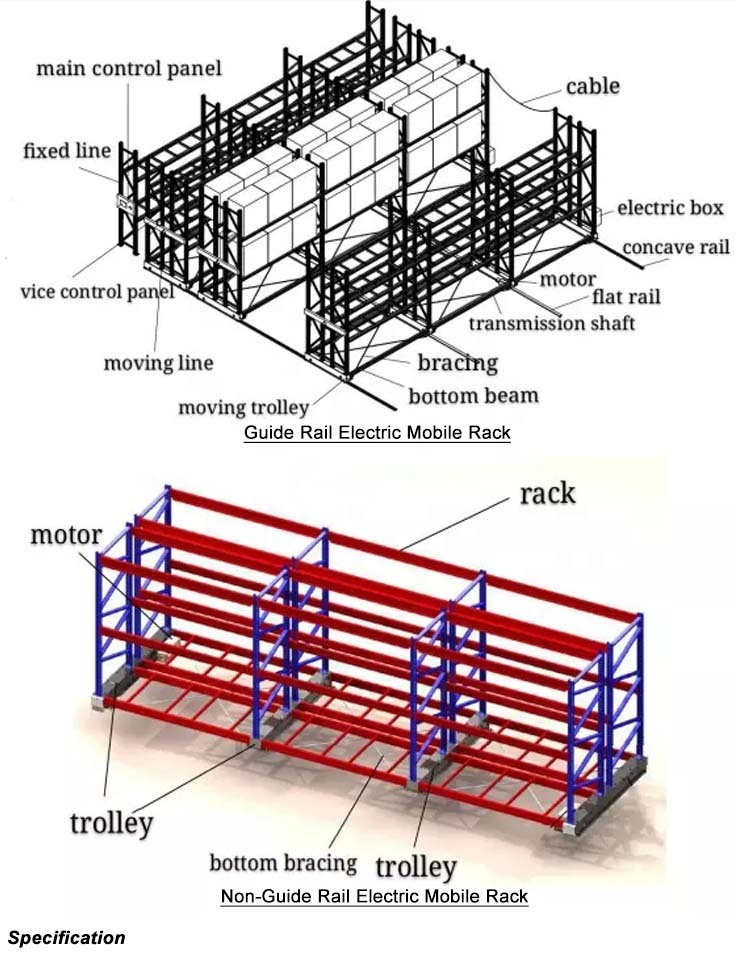
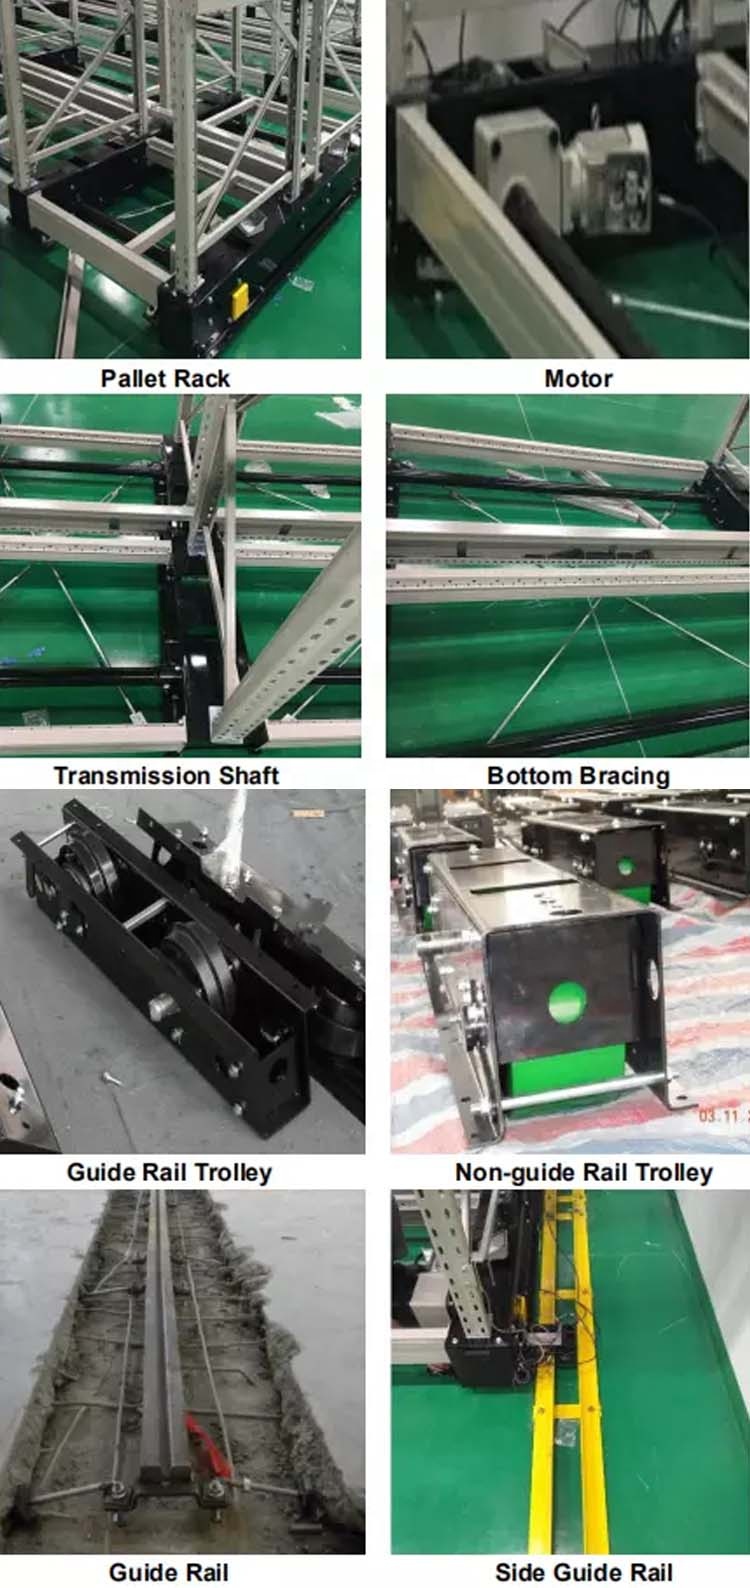
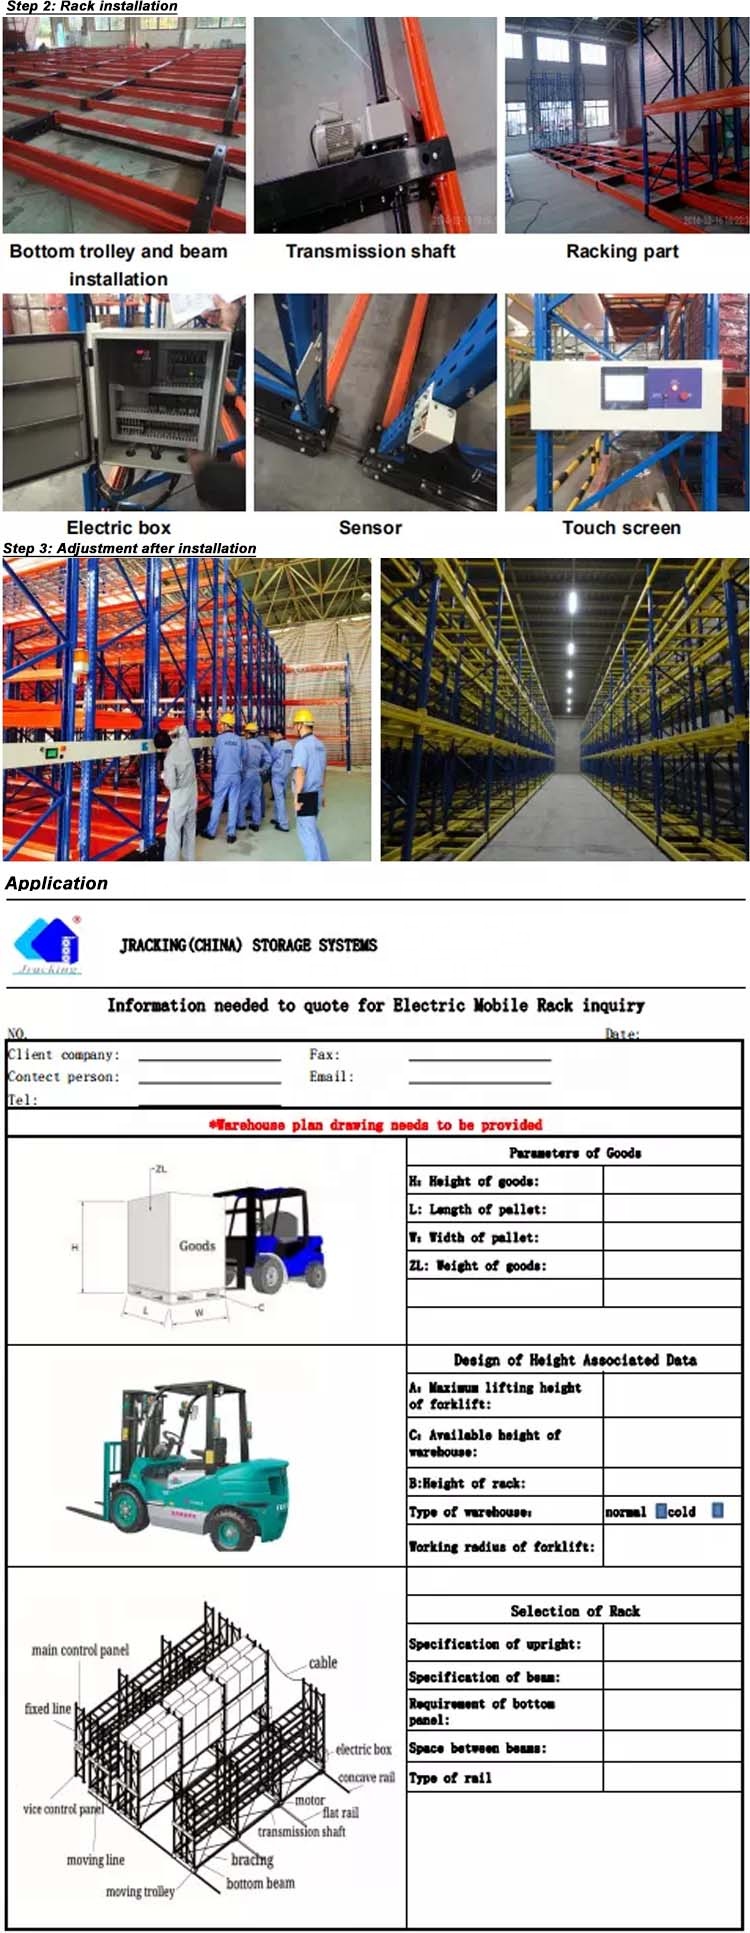
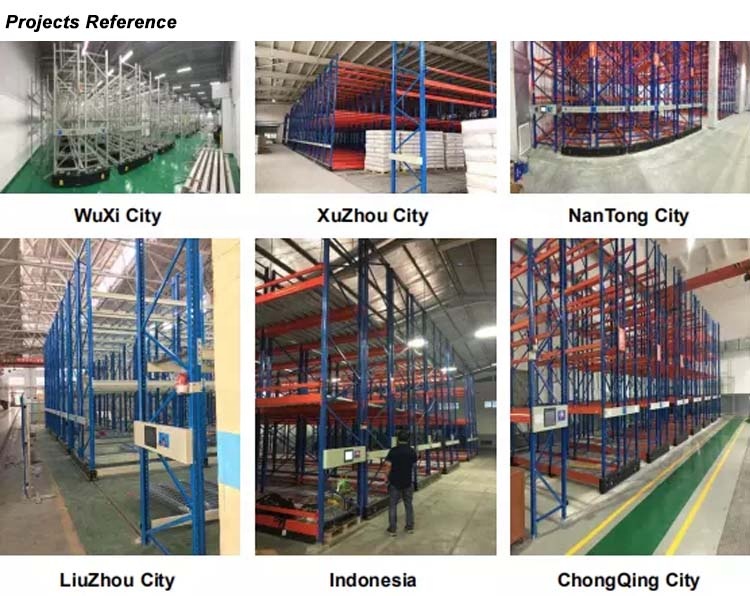
An electric mobile racking system consists of heavy-duty pallet racks mounted onto motorized mobile bases. These bases run on embedded or surface-mounted tracks and can be controlled via buttons or software to open specific aisles when access is needed.
Q2: What is the main difference between Guide Rail and Non-Guide Rail systems?
The Guide Rail system requires floor slotting and offers higher load capacities (up to 32 tons/unit). The Non-Guide Rail system uses polyurethane wheels and mechanical guidance, eliminating the need for concrete trenching, making it suitable for lower load requirements (up to 16 tons/unit) or rented premises.
Q3: Can mobile racking systems be used in cold storage warehouses?
Yes. Electric mobile racking is ideal for cold storage and deep-freeze environments because it maximizes space utilization up to 85%, significantly reducing cooling energy costs per pallet stored.
Q4: Are electric mobile racks safe for warehouse operators?
Absolutely. Every mobile racking unit is equipped with optical sensors, emergency stop devices, photoelectric safety barriers, and mechanical protection devices to ensure full operator and forklift safety.
Q5: What certifications do your racking products hold?
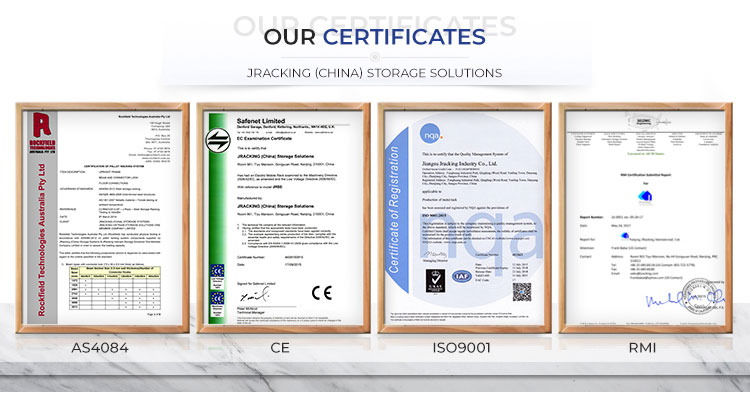
Our products comply with international quality and safety standards, certified under ISO9001:2008 and European CE regulations.
Q6: Is customization available for specific warehouse dimensions?
Yes, all specifications including depth, height, width, frame loading, and color can be tailored according to your warehouse layout and operational demands.